Differential pressure can mislead when it is treated as an isolated number. The same filter presents different resistance at different airflows. Maintenance teams need a trend under comparable conditions, a record that identifies what was installed where, and a method for investigating abrupt changes.
This guide covers all three: reading pressure logs, building a filter register that stays traceable, planning maintenance stage by stage, and the limits of what any pressure reading can tell you.
Establish a Baseline After Installation
Record the date, unit operating condition and airflow where available. Confirm that the pressure taps represent the intended filtration stage: a reading across several stages should not be labelled as the drop of one element. Identify the instrument and its measurement range in the record.
Where the element is new, the manufacturer initial pressure drop value belongs to a stated airflow and face size. Comparing a site reading with a catalogue figure taken at a different flow is not a like-for-like comparison.
Check Operating Changes Before Interpreting a Rise
Has fan speed, damper position or airflow changed? Was the previous reading taken under comparable conditions? Only then investigate dust loading, moisture, an incorrect element or measurement-line problems.
One high reading may be insufficient for a replacement decision. Acceptance limits depend on the product and the system procedure, not on a number copied from another site.
Do Not Treat a Sudden Fall as Automatic Improvement
Reduced airflow, a disconnected sensing tube or a measurement error can all lower the reading. A displaced element or leakage around its frame is another possibility worth investigating. Check operating conditions and installation before interpreting the result, because low differential pressure does not establish filtration performance. Air that bypasses the element through a poor seal shows up as less resistance, not more.
Field example. If the fan switches to reduced operation after a reading, do not compare the next low pressure value directly with the earlier high-flow reading. Restore comparable conditions or label the difference. This avoids interpreting an operating change as recovery of the filter.
Pair Trend Readings With Action Records
Log date, operating condition, value and any maintenance action. Verify suspicious measurements before including them in a trend. Apply manufacturer guidance, system limits and the site maintenance procedure together. When the filter class or installation interface changes, do not transfer the old element baseline to the replacement without review.
Build a Filter Register That Stays Traceable
A site can use filters with identical outside dimensions but different classes or seals. A stock list based only on size loses that distinction. A register should show where an element is installed and which approved specification governs its purchase.
Give each unit and stage a stable identity
Assign a unit reference to each air handling unit or housing and identify every filtration stage, recording the number of elements in that stage. Keep the reference stable when equipment moves and update its location separately, so earlier maintenance notes stay connected to the same equipment.
Separate specification from stock information
The approved specification should include class, standard, dimensions, airflow, frame, seal and drawing revision. The stock record holds quantity, storage location, batch details and purchase order reference. If a supplier changes its part number, keep a cross-reference and check technical equivalence separately: a new code is not by itself a new specification.
Record replacements consistently
Capture installed and removed part numbers, date, responsible person and reason for replacement. Pressure readings need an operating condition or airflow reference. Link any required acceptance records. Mark missing measurements as not recorded rather than entering zero, which could later be mistaken for an actual reading.
Use the records to inform future orders
Review repeated early changes by unit and stage. Assess spare stock against past consumption, planned shutdowns and confirmed supply lead times. Maintenance history alone is not a service-life guarantee, but the register makes decisions traceable and helps buyers order the current approved revision rather than whatever was delivered last time.
Field example. A usable record chain runs unit, then stage, then approved element, then purchase order, then receiving, then installation, then replacement reason. Track location through that chain rather than through a shelf label alone, and preserve dated changes instead of deleting old entries so previous decisions can be reviewed.
Plan Maintenance Stage by Stage
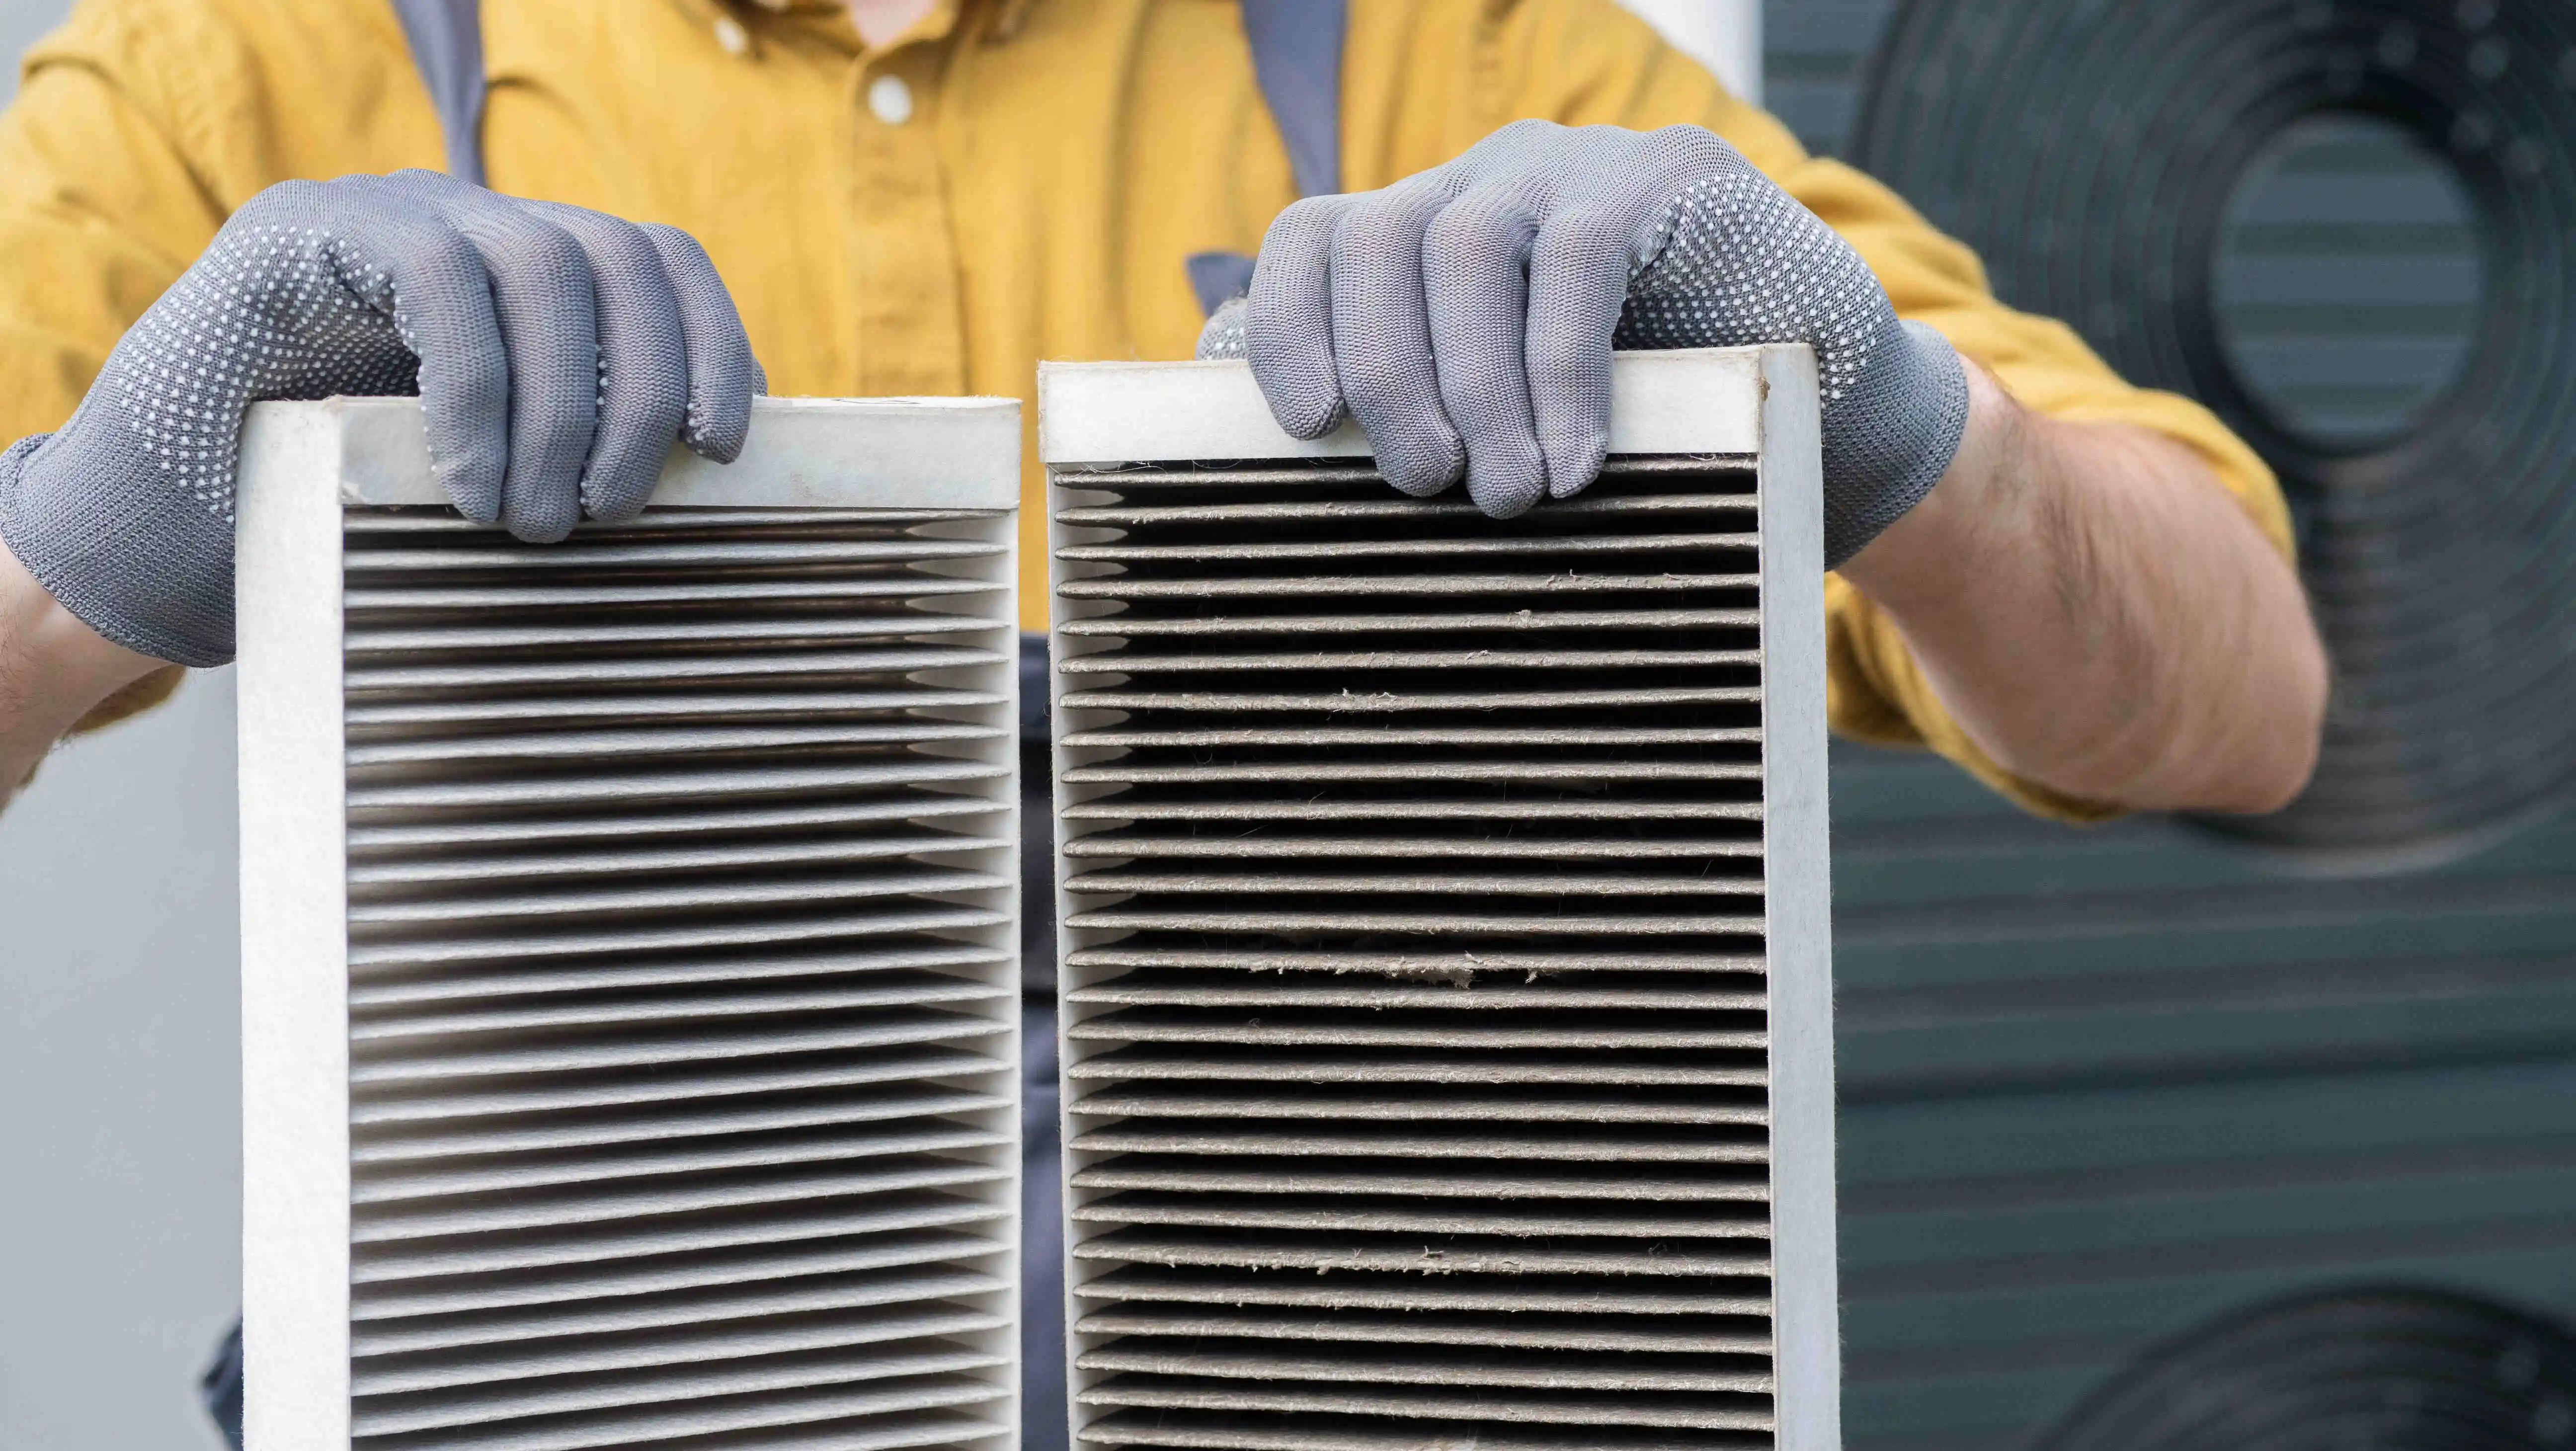
The prefilter is one of the first stages in an air handling system, and neglecting it affects the loading of everything downstream. A maintenance plan needs more than a date on a calendar: product condition and unit operation have to be tracked together.
Map the stages of each unit
Record prefilter, main filter and any final high-efficiency stage separately, listing element quantities and part numbers. Identify readings that span several stages. When transferring an interval from one unit to another, do not assume outdoor dust loading and operating hours are identical.
Combine scheduled inspections with condition checks
Set inspection dates and support them with pressure and physical-condition records. Construction dust, a nearby process change or longer operating hours may justify extra checks. Replacement limits should follow product instructions and site procedures; a fixed number of months is not a universal service life.
Make installation problems visible
Inspect seating, seals and retention. Air bypassing the frame undermines the prefiltration stage even when the element itself is sound. When torn media or an incorrect element is found, record the cause as well as the replacement date. Repeated faults call for a review of supply, transport or installation practice rather than another replacement.
Review downstream effects using the records
Keep upstream and main-stage histories under the same unit reference. Investigate operating conditions when early loading or unusual pressure trends appear. More frequent prefilter replacement is not automatically economical: element cost, maintenance work and system behaviour have to be evaluated together. Cleaning or washing should only be considered where the specific product instructions permit it, which is a narrower case than it is often assumed to be and is covered in washing and service life.
Field example. Construction near a site is followed by early loading. Record the start of the temporary challenge and review inspection frequency, instead of permanently shortening every interval. Reassess after the work ends and examine downstream records for the same period.
What Pressure Records Cannot Tell You: the Gas-Phase Stage
Low or unchanged differential pressure does not establish the remaining gas-removal capacity of an activated carbon stage. Pressure readings concern airflow resistance; target-gas performance needs its own assessment. This is the most common reason a carbon stage is reported as working when the odour has already returned.
Odour downstream of a carbon filter does not always mean the carbon is simply old. Review these separately rather than reordering the same cartridge:
- Gas compatibility. Activated carbon does not retain every gas with the same capacity. The adsorbent has to match contaminant identity, concentration and process conditions. Some applications need treated media, and a generic cartridge should not be assumed suitable for all VOCs or odours.
- Consumed capacity. The target contaminant appears downstream as capacity is used. Do not base replacement only on elapsed months or on smell; combine an appropriate measurement method, operating history and product instructions, and compare commissioning and current results under equivalent conditions. A cartridge that looks clean from the outside tells you nothing about its remaining gas capacity.
- Airflow change. Higher airflow changes the contact conditions assumed in the filter assessment. Do not reduce airflow arbitrarily: the technical team has to weigh ventilation and process requirements.
- Bypass. Air travelling around rather than through the element affects removal. Inspect fan settings, covers, connections, seals and seating surfaces, and establish the correct flow path before ordering new carbon as the assumed solution.
- Humidity, temperature and condensation. Relative humidity and temperature affect adsorption depending on gas and media. Record condensation or wetting, and request the applicable range rather than applying one limit to every carbon product. Drying, washing or field regeneration should not be improvised without product instructions.
- Prefiltration. If dust or aerosols are carried into the stage, review the upstream particulate filtration.
- Process loading. New chemicals, higher production, longer shifts or concentration peaks can invalidate the assumptions the original selection was based on.
| Observation | First investigation area |
|---|---|
| Insufficient performance from day one | Gas identity, adsorbent, airflow and bypass |
| Odour returns after a period | Capacity, peak loading and process changes |
| Performance changes on humid days | Humidity, temperature and condensation |
| Pressure unchanged but measured gas rises | Gas-phase performance and replacement criteria |
Smell is not a measurement proving that a gas is absent or at a safe concentration, and reduced smell alone should not determine health or process-safety decisions. Where data is absent, identify the measurement need rather than guessing.
Field example. A filter previously operated under accepted conditions, but the shift was extended and a new cleaning chemical introduced. Instead of immediately reordering the same cartridge, record the changed substances and hours, assess the current gas challenge using an appropriate method, then review media and capacity selection. This is a constructed example of the investigation sequence, not a documented customer case.
Practical Checklist
- Consistent pressure taps, operating conditions and identified instrument.
- Fan, damper and airflow changes checked before interpreting any trend.
- Sensing lines and installation condition inspected on an unexplained fall.
- Unit reference, stage, element count and approved drawing revision in the register.
- Stock, batch and purchase reference kept separate from the specification.
- Replacement reason and measurement conditions recorded; missing values marked as not recorded.
- Stage map per unit, with linked upstream and downstream histories.
- Gas-phase stages assessed by an appropriate method, not by pressure or smell.
When a replacement reveals that the installed element never matched the approved specification, the correction belongs in the next request document rather than in a verbal note to the supplier. Send the manufacturer the dimensions, requested class, airflow per element and quantity, and identify missing information so assumptions can be reviewed explicitly.
Request a technical quotation · Our air filter manufacturing in Turkey · Catalogues and technical documents
Frequently Asked Questions
No. First confirm that fan speed, damper position and airflow are comparable to the previous reading, and that the pressure taps cover only the stage in question. A single high value under changed operating conditions is not a replacement decision. Acceptance limits come from the product instructions and the site maintenance procedure.
No. A low reading can also indicate reduced airflow, a disconnected sensing tube, a measurement error, a displaced element or air bypassing the frame. Pressure describes airflow resistance, not filtration performance, and for an activated carbon stage it says nothing about the remaining gas-removal capacity.